One size
doesn't
fit all.
We don't optimize the old. We put something new on the table. Open-source 3D printable gadgets designed collaboratively by our community. Fork it, modify it, make it yours.
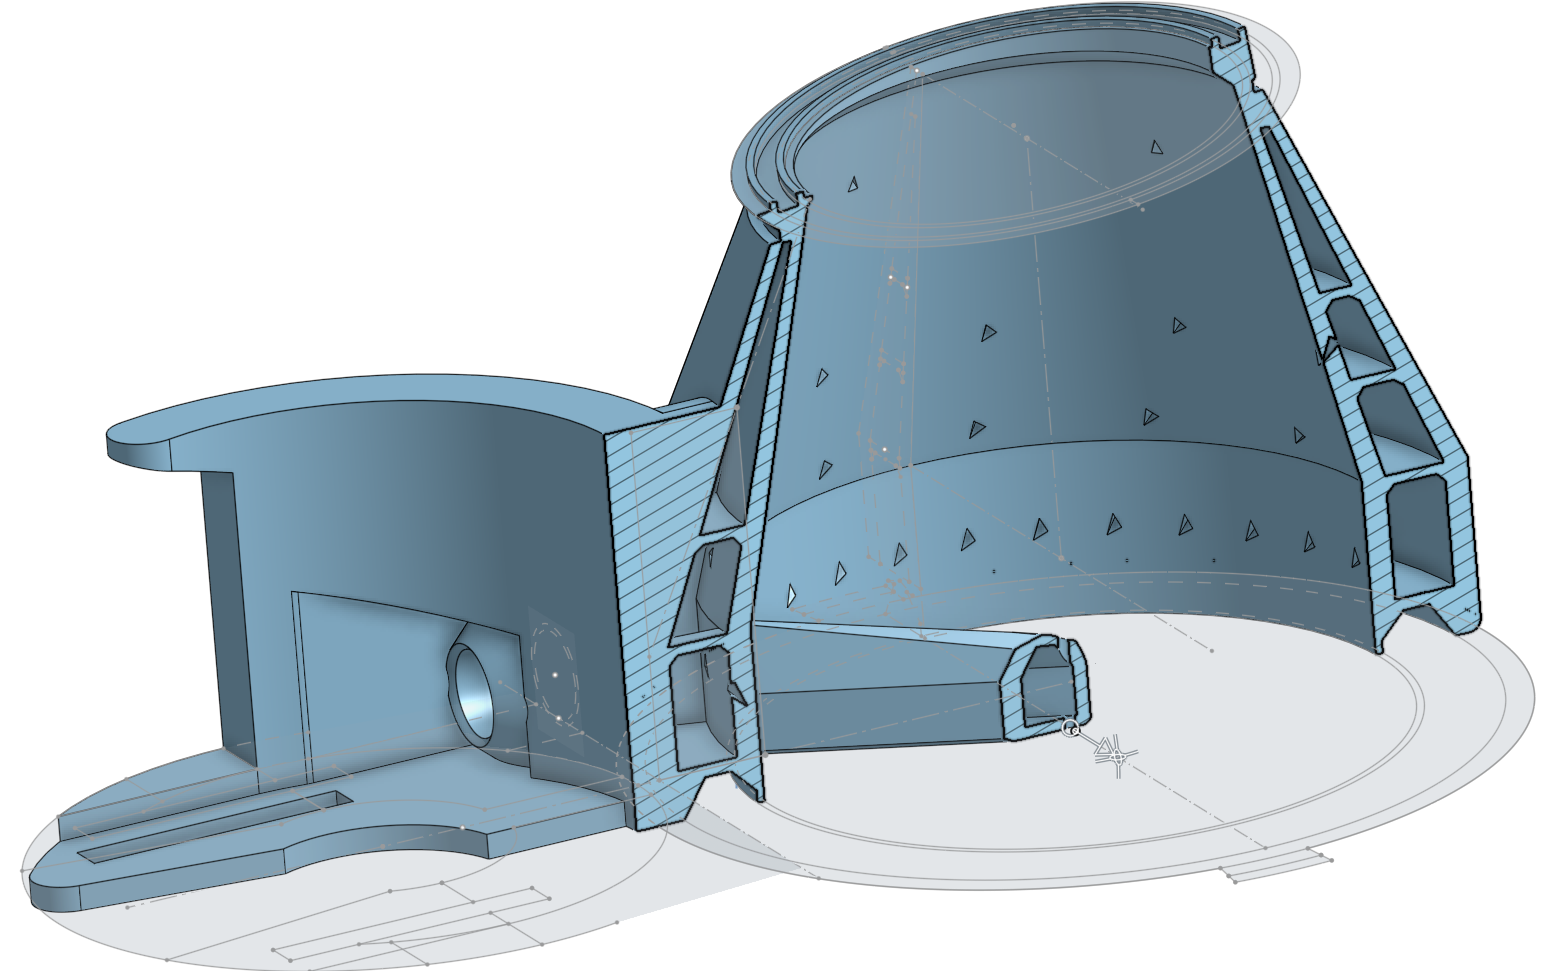
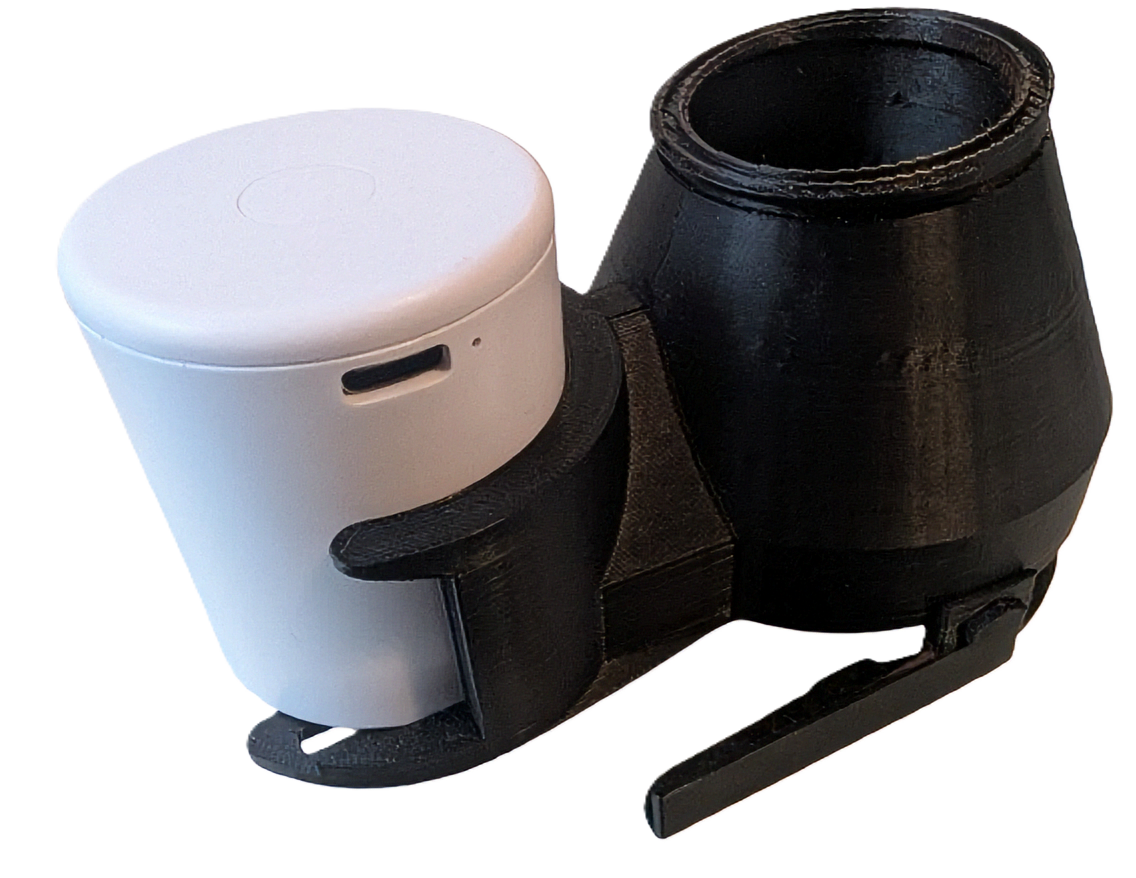 AIRSHAKER / REV C 0.4mm · PETG-HF
System Identification
MF AirShaker Rev C
The first product in the espresso gear line. A 3D printable tool that uses precision air channels to distribute coffee grounds evenly in the puck — replacing mechanical WDT tools entirely. Novel category. Better taste in the cup, even with a cheap grinder.
| DISTRIBUTION METHOD | Precision Air (Vortex) |
|---|---|
| REPLACES | WDT + Manual Distribution |
| MATERIAL PROTOCOL | PETG-HF |
| PRECISION TOLERANCE | +/- 0.05 mm |
| LAYER HEIGHT OPT | 0.4 mm |
| ESTIMATED PRINT | 2h 14m @ 250mm/s |
| PRODUCT CATEGORY | New Category (Novel) |
| LICENSE | CERN-OHL-S (Open Source) |
Why We Exist
We put something
new on the table.
MakerFirst exists because the best 3D printable gadgets haven't been designed yet. We don't make the thing that already exists, slightly cheaper. We invent categories that didn't exist, then open source the blueprints.
Partners, not consumers
We don't ship products to customers. We release designs to partners. Every maker who prints, modifies, or improves our work is a collaborator. Your fork is as valid as our main branch.
New categories, not better clones
Optimization of existing ideas is not our thing. The AirShaker didn't exist before we made it — a new product category born from a different way of thinking about the problem.
Open by default
Every design file, every iteration, every mistake — public. CERN-OHL-S license. Take it, fork it, sell it, improve it. The only requirement is you pass the same freedom forward.
Built for real printers
No idealized designs that only work on industrial machines. Our files are tested on Bambu, Prusa, and Voron. PETG-CF and PA12-CF protocols included. If your printer can do 0.12mm layers, you can build this.
Commit History
Active Branches
wide-base-v1.2
Wide-base variant for 58.5mm baskets. Industrial espresso machine fit.
zero-static-mod
Conductive filament integration. Eliminates static cling in dry environments.
dnse-diffuser-alpha
Dense diffuser pattern test. Experimental — needs more data on extraction uniformity.
Assembly Instructions
Build It Yourself.
Every design comes with complete slicing profiles, material specs, and assembly notes. Print it today. Use it tomorrow.
Slicing Protocol
Use high-temperature PETG-CF. 3 wall loops minimum for structural integrity. Infill: 25% Gyroid. No support required for internal air channels. Slice at 0.16mm for the best balance of speed and surface quality.
Print & Post-Process
Heat-treat parts at 65°C for 2 hours to relieve internal printing stresses. Surface finish should be matte to reduce static cling. Remove any stringing from air channel openings with a fine needle.
Final Assembly
Press-fit the bearing into the upper housing. Secure with M3x12 socket head screws. Torque to exactly 1.2Nm. The AirShaker snaps together — no glue needed, no permanent commitment.
Get Involved
Print. Fork. Improve.
Every MakerFirst design is open source. Download the files, slice them your way, and if you improve something — push it back. We're partners, not customers.
All files released under CERN-OHL-S license · makerfirst.ca